High-Speed Hardened Steel Turning: Tooling, Speed & Spindle Optimization (HRC 45-65)
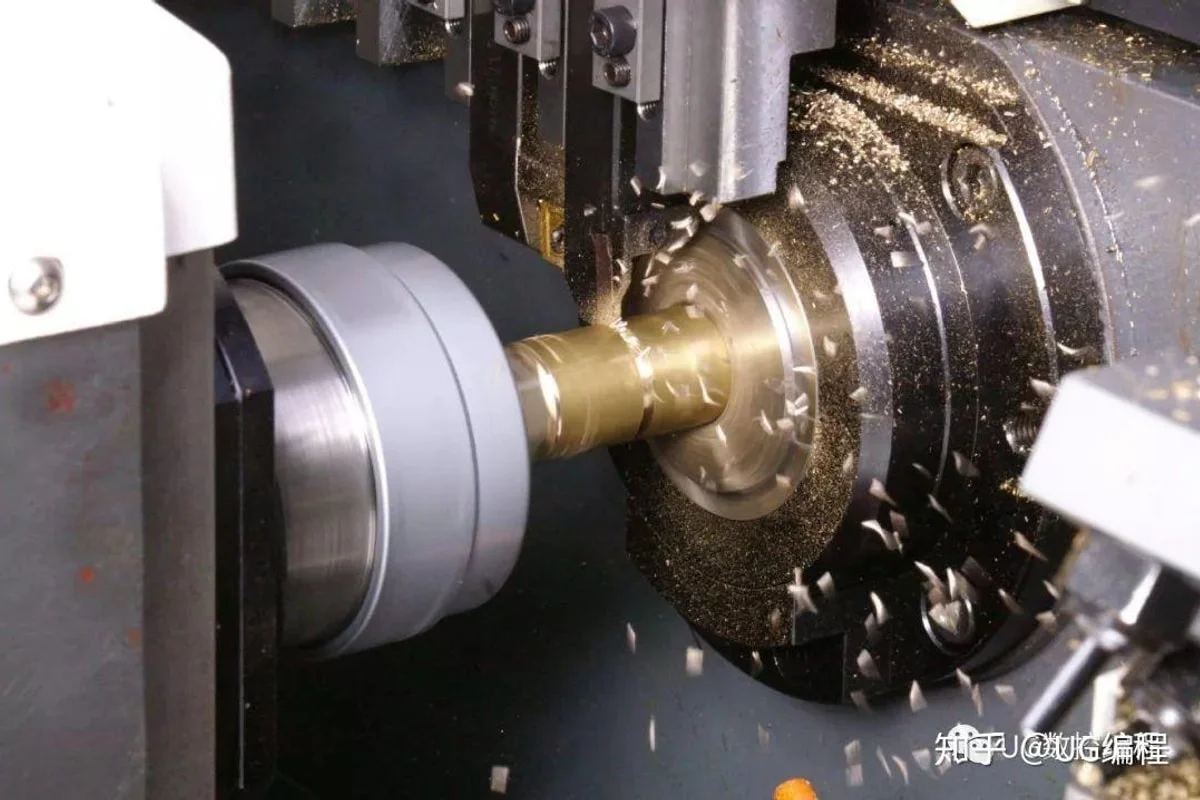
In modern mechanical manufacturing, hard turning—the process of single-point turning hardened steel workpieces between 45 HRC and 65 HRC—has become a disruptive replacement for slow, expensive cylindrical grinding operations.
By performing finish turning on a rigid CNC lathe (such as the DAHAN TCK50 or CK6150), shops achieve dimensional tolerances within ±0.005 mm and surface roughness finishes as fine as Ra 0.2 - 0.4 µm, while cutting cycle times by up to 60%.
1. Machine Tool Requirements for Hard Turning
You cannot perform hard turning on a lightweight or worn lathe. The extreme cutting resistance of hardened alloys exerts high radial forces back into the tool post and headstock.
The machine must possess:
- Exceptional Dynamic Rigidity: Heavy Meehanite cast iron beds that dampen high-frequency chatter.
- Zero-Backlash Axis Movement: Pre-tensioned C3 class ground ball screws with direct-coupled digital AC servomotors.
- High Spindle Stiffness: Spindles equipped with pre-loaded angular contact ball bearings and double-row cylindrical roller bearings with runout under 0.003 mm.
2. Tooling Selection: Polycrystalline Cubic Boron Nitride (PCBN) vs. Ceramics
When turning hardened steels, conventional carbide inserts fail rapidly due to thermal wear. Specialized super-hard cutting materials are mandatory:
PCBN (Polycrystalline Cubic Boron Nitride)
- Hardness: Second only to diamond, but chemically stable with iron-based alloys at high cutting temperatures (up to 1,200°C).
- Application: Ideal for continuous and lightly interrupted cuts in hardened alloy steels (AISI 4140, 4340, 52100, D2) above 55 HRC.
- Insert Edge Preparation: Always choose a honed (chamfered + radius) edge prep (e.g., 0.1mm × 20° T-land) to prevent chipping of the brittle cutting edge.
Mixed Ceramics (Al₂O₃ + TiC)
- Application: Economical alternative for smooth continuous turning of case-hardened shafts and bearing rings where thermal shock is low.
3. Recommended Cutting Parameters
| Workpiece Material | Hardness | Insert Grade | Cutting Speed (Vc) | Feed Rate (f) | Depth of Cut (ap) |
|---|---|---|---|---|---|
| 52100 Bearing Steel | 60 - 64 HRC | Tipped PCBN | 120 - 180 m/min | 0.08 - 0.15 mm/rev | 0.10 - 0.25 mm |
| 4140 Induction Hardened | 50 - 55 HRC | Mixed Ceramic | 140 - 220 m/min | 0.10 - 0.20 mm/rev | 0.15 - 0.35 mm |
| D2 Cold Work Tool Steel | 58 - 62 HRC | High-CBN Content | 90 - 140 m/min | 0.06 - 0.12 mm/rev | 0.08 - 0.20 mm |
4. Wet vs. Dry Cutting in Hard Turning
Unlike conventional soft turning, hard turning is predominantly performed DRY:
- Thermal Shock Hazard: Flooding the cutting zone with cold coolant causes cyclic thermal shock on the red-hot PCBN tip, leading to micro-cracking and catastrophic insert breakage.
- If coolant is essential for workpiece dimensional stability, it must be applied as high-pressure through-tool coolant (≥ 20 Bar) aimed directly into the tool-chip interface.
Summary & Shop Recommendations
Hard turning on DAHAN CNC lathes delivers dramatic cycle time reductions, superior geometric concentricity, and eliminates the need for costly secondary grinding operations.
To consult with our cutting tool application engineers regarding your hardened component drawings, reach out directly to xiuc32860@gmail.com.
Discuss Your Production Goals with DAHAN Engineers
Submit your component drawings for tooling selection, cycle time estimation, and direct factory pricing.
Запрос технического предложения и цены от завода
Прямая заводская цена FOB Циндао или CIF с доставкой в ваш порт за 2 часа. Отправьте чертежи деталей для оценки нашими инженерами.